Leave Your Message
Choosing among China’s top Laser Head suppliers requires more than comparing prices and power ratings. The right supplier should match your material, laser source, machine platform, and production goals. A head designed for thin stainless steel may perform poorly on thick carbon steel. Small details matter, too, including nozzle alignment, protective-window access, cooling stability, and focal-position accuracy.
Dr. Stefan Kaierle, a respected laser-processing specialist, has emphasized this practical principle: “Process quality depends on the complete system, not the laser source alone.” That view is useful when evaluating Chinese manufacturers. Ask for test-cut records, beam-diameter data, compatible wavelengths, and verified operating ranges. Request close photographs of internal optics, cable connections, seals, and cooling channels. Reliable suppliers should explain these details clearly.
Look for evidence from real installations. A supplier with documented customer cases, traceable components, responsive engineers, and local service support usually deserves closer attention. Check whether the Laser Head supports your controller, cutting software, piercing strategy, and planned duty cycle. Warranty terms need careful reading. “Fast support” means little without response times and spare-part availability.
Do not choose only by catalog claims. Test first. A sample cut may reveal unstable kerf width, excessive dross, or inconsistent piercing. I have seen attractive specifications hide practical weaknesses. That is uncomfortable, but worth admitting. Supplier selection is partly technical judgment and partly disciplined skepticism. The best choice balances optical performance, mechanical durability, integration effort, maintenance access, and long-term operating cost.
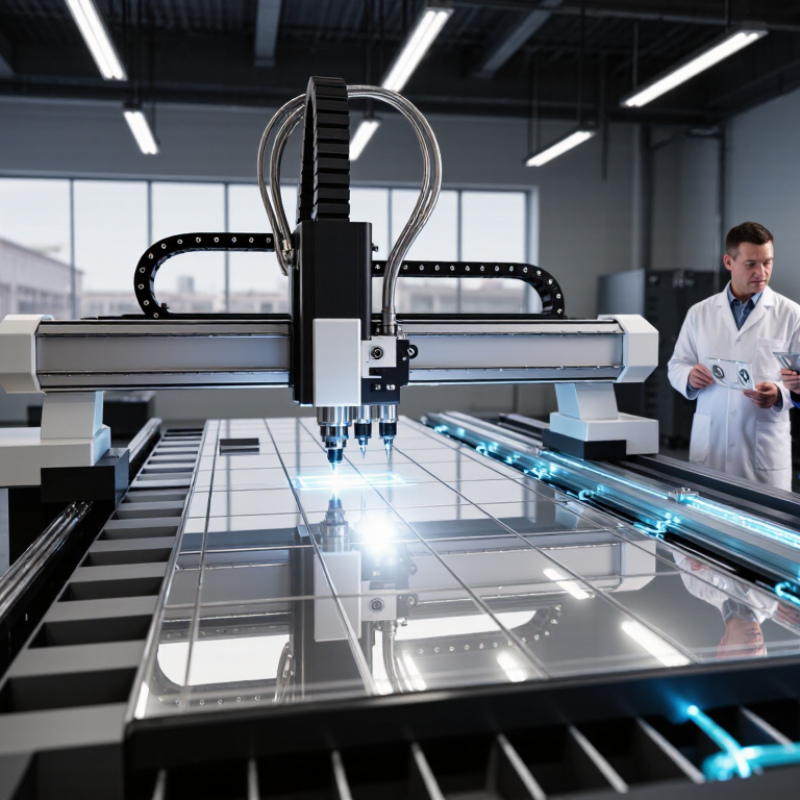
China Top Laser Head Suppliers: How to Choose?
A laser head is the working interface between the source and the material. Most industrial fiber systems operate around 1064–1080 nm. This range suits common metal cutting, welding, and surface treatment applications. However, wavelength compatibility must match the laser source, optics, coatings, and protective window. A small mismatch can reduce transmission and shorten service life. It happens more often than buyers expect.
Power ratings usually range from 1 to 30 kW. Higher power does not automatically produce better results. A 6 kW head may be practical for regular steel cutting, while thicker materials may require a stronger thermal design. Check the rated power, continuous operating limits, cooling method, focal adjustment, nozzle stability, and sensor protection. Ask suppliers for measured test data, not only catalog figures. Factory inspection records and application trials provide stronger evidence. In my experience, incomplete cooling details are a warning sign. Still, even experienced teams can select a head that is too powerful for their actual workload.
Tips: Confirm the 1064–1080 nm range first. Match the head to real power demand. Request cutting or welding samples using your material. Check replacement window costs and delivery time. Review technical support before ordering. A supplier with clear drawings, test reports, and traceable quality records is usually easier to trust.
| Selection Dimension | Typical Range or Specification | Why It Matters | Practical Selection Guidance |
|---|---|---|---|
| Operating Wavelength | Typically 1064–1080 nm for fiber-laser processing | The optical coating, protective window, focusing optics, and monitoring components must be compatible with the laser wavelength. | Confirm the head is specified for the actual laser source wavelength and not only for a general “fiber laser” category. |
| Rated Laser Power | Approximately 1–30 kW, depending on the head design | Higher power increases thermal load, back-reflection risk, contamination sensitivity, and cooling requirements. | Choose a continuous-power rating with a reasonable operating margin rather than selecting a head at its absolute limit. |
| Processing Type | Cutting, welding, cladding, hardening, brazing, or additive manufacturing | Different processes require different focal lengths, gas delivery, working distances, spot shapes, and adjustment ranges. | Select a process-specific optical configuration instead of using one general-purpose head for every application. |
| Focusing Optics | Common focal lengths include approximately 100–300 mm; larger systems may use longer focal lengths. | Focal length affects spot size, depth of focus, working distance, and accessibility around the part. | Use shorter focal lengths for compact, fine-feature work and longer focal lengths where working distance or process clearance is important. |
| Beam Delivery | Fiber-coupled input with process fibers commonly selected by core diameter and numerical aperture | The input fiber and optical design determine achievable spot size, beam quality, and compatibility with the laser system. | Match fiber connector type, core diameter, numerical aperture, and beam parameter requirements before ordering. |
| Spot Size | Application-dependent; commonly ranges from sub-millimeter spots to several millimeters | Spot size influences energy density, penetration, heat-affected zone, processing speed, and surface finish. | Verify the spot-size range at the stated fiber, focal length, and power conditions; do not rely on nominal lens diameter alone. |
| Beam-Shaping Capability | Circular, rectangular, adjustable, ring-shaped, or other tailored intensity profiles | Beam shaping can improve weld stability, reduce spatter, control penetration, or support high-speed surface processing. | Use a simple circular profile for conventional cutting and consider shaped beams for demanding welding, cladding, or heat-treatment processes. |
| Protective Window | Replaceable optical window, usually with contamination monitoring on higher-power systems | Spatter, smoke, and dust can damage focusing optics and reduce transmission efficiency. | Check window material, dimensions, coating range, replacement procedure, sealing method, and availability of qualified spares. |
| Cooling Method | Air cooling for lower-power designs; water cooling is common for sustained high-power operation | Cooling maintains optical alignment and limits thermal drift during continuous processing. | For high-duty-cycle or multi-kilowatt applications, verify coolant flow, pressure, temperature, connector type, and alarm requirements. |
| Assist-Gas Delivery | Coaxial, side, or multi-jet gas delivery; configuration depends on the process | Gas flow affects oxidation, spatter removal, shielding, penetration, and cut quality. | Confirm nozzle geometry, gas inlet size, pressure range, flow direction, and compatibility with oxygen, nitrogen, argon, or process-specific gases. |
| Working Distance | Often tens of millimeters, determined by focal length and nozzle design | The correct distance is needed to achieve focus and maintain stable gas coverage without collision risk. | Select a head whose working-distance range fits the machine structure, part geometry, height variation, and automation tolerances. |
| Height Sensing | Capacitive sensing, laser triangulation, or external machine-axis control | Automatic height control helps maintain focus and protects the nozzle when part flatness varies. | Confirm sensor material limits, response speed, control interface, calibration method, and compatibility with the machine controller. |
| Back-Reflection Protection | Optical isolation, monitoring, and interlock functions may be included | Highly reflective materials can send energy back toward the head or laser source, creating safety and reliability risks. | Ask for the allowable reflection conditions, alarm thresholds, response time, and recommended material limitations. |
| Mechanical Interface | Mounting flange, robot adapter, CNC interface, and nozzle assembly vary by design | Mechanical compatibility determines installation time, rigidity, alignment accuracy, and collision clearance. | Request dimensional drawings, center-of-gravity data, mounting-hole patterns, cable routing details, and total head mass. |
| Automation Compatibility | CNC, robotic, gantry, and specialized motion platforms | The head must integrate with motion limits, cable chains, process signals, safety circuits, and control software. | Validate I/O signals, fieldbus or analog interfaces, emergency-stop behavior, and cable bend radius with the system integrator. |
| Serviceability | Replaceable nozzles, windows, seals, lenses, and sensor components | Consumable replacement time and spare-part cost directly affect equipment availability. | Compare maintenance intervals, spare-part lead times, cleaning procedures, technical documentation, and remote support. |
| Acceptance Testing | Optical inspection, power test, cooling test, gas test, focus verification, and sample processing | Testing confirms that the supplied head meets the stated optical, mechanical, and process requirements. | Define measurable acceptance criteria before purchase, including power level, focal position, spot size, gas flow, and continuous operating time. |
Note: Actual specifications vary by optical configuration, laser source, process material, duty cycle, and machine integration. Always verify the latest technical datasheet and conduct application testing before final selection.